Home / PRODUCT
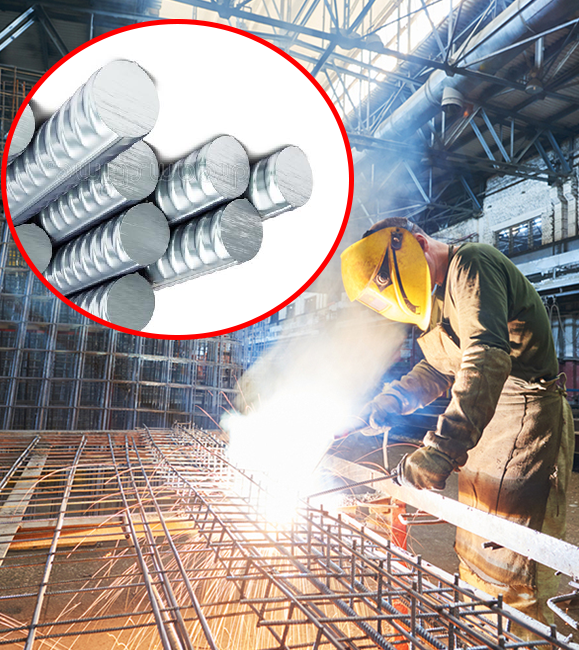
Aman Rolling Mills bars or Thermo-Mechanically Treated bars are high-strength reinforcement bars having a tough outer core and a soft inner core. The first step of the manufacturing process involves formation of billet through Continuous Casting Machine (CCM). CCM is a process of casting metal into billet which can be further shaped into suitable products. At Aman Rolling Mills TMT we believe in being a class apart, we have a well-equipped integrated plant that produces billets, in – house and thereafter the process of making Aman Rolling Mills begins. The Aman Rolling Mills is passed through quinching and tempered process. While passing the Aman Rolling Mills through the quinching and tempered process, the water pressure is optimised. The sudden quenching and drastic change in temperature toughens the outer layer of the Aman Rolling Mills bar, thus making it super tough and durable.Once this process is over, the Aman Rolling Mills bars are subject to atmospheric cooling. This is done in order to equalise the temperature difference between the soft inner core and the tough exterior. Once the Aman Rolling Mills bar cools down, it slowly turns into a ferrite-pearlite mass. The inner core remains soft giving the Aman Rolling Mills bar great tensile strength, shock absorbing resistance and elongation point. This design is unique to the Aman Rolling Mills bars and gives superior ductility to the bars. Also, this unique manufacturing technology of V Rib and the absence of Cold stress makes this bar corrosion-resistant and also boosts its weldability.
| Size | Specified (kg/meter) | Specified (kg/meter) | Per Wt.Variation (kg/meter) | Individual sample variation | |||
|---|---|---|---|---|---|---|---|
| ISI Std. | Aman Rolling Mills Std. | ISI Std. | Aman Rolling Mills Std. | ISI Std. | Aman Rolling Mills Std. | ||
| 08mm | 0.395 | 367 to 423 | 379 to 411 | 0.056 | 0.032 | ±7 | ±5 |
| 10mm | 0.617 | 574 to 660 | 598 to 636 | 0.086 | 0.038 | ±7 | ±4 |
| 12mm | 0.888 | 844 to 932 | 870 to 906 | 0.088 | 0.036 | ±5 | ±3 |
| 16mm | 1.580 | 1501 to 1659 | 1548 to 1612 | 0.158 | 0.064 | ±5 | ±3 |
| 20mm | 2.470 | 2396 to 2544 | 2445 to 2495 | 0.148 | 0.050 | ±3 | ±2 |
| 25mm | 3.850 | 3735 to 3965 | 3811 to 3889 | 0.230 | 0.078 | ±3 | ±2 |
| 28mm | 4.830 | 4685 to 4975 | 4782 to 4878 | 0.290 | 0.096 | ±3 | ±2 |
| 32mm | 6.314 | 6125 to 6503 | 6207 to 6884 | 0.290 | 0.096 | ±3 | ±2 |
| Chemistry | Unit | IS 1786 Fe 415 | Aman Rolling Mills Fe 415 | Aman Rolling Mills Fe 500 | Aman Rolling Mills Fe 550 |
|---|---|---|---|---|---|
| Carbon | % | 0.30 Max | 0.25 Max | 0.20 Max | 0.20 Max |
| Sulphur | % | 0.06 Max | 0.05 Max | 0.05 Max | 0.05 Max |
| Phosphorus | % | 0.06 Max | 0.05 Max | 0.05 Max | 0.05 Max |
| S & P | % | 0.11 Max | 0.10 Max | 0.10 Max | 0.10 Max |
| Mechanical Properties | Indian Standards (IS:1786) | American Standards (ASTM A 615) | European Standards (DIN 488) | Aman Rolling Mills Standards |
|---|---|---|---|---|
| Grade | Fe 415 | 60 (420) | Bst-420 S | |
| Proof stress in N/mm2 | 415 | 420 | 420 | 425 |
| Tensile strength in N/mm2 | 485 | 500 | 500 | 490 |
| Elongation in % | 14.5 | 14 | 10 | 17 |
| Bend Test | up to 22 mm -3D | 10 to 16 mm -4D | 6 to 25 mm -4D | 4D |
| Grade | Fe 500 | 75 (520) | Bst-500 S | |
| Proof stress in N/mm2 | 500 | 520 | 500 | 525 |
| Tensile strength in N/mm2 | 545 | 620 | 550 | 620 |
| Elongation in % | 12 | 9 | 10 | 15 |
| Bend Test | up to 22 mm -4D | 10 to 25 mm -4D | 6 to 25 mm -5D | 4D |
| Grade | Fe 550 | 90 (570) | Bst-500-m | |
| Proof stress in N/mm2 | 550 | 570 | 500 | 570 |
| Tensile strength in N/mm2 | 585 | 570 | 550 | 690 |
| Elongation in % | 8 | 7 | 8 | 10 |
| Bend Test | up to 22 mm -5D | 10 to 25 mm -5D | 6D | 5D |